High-Performance Cable Glands & Industrial Connectors
Engineered for high-ampacity electrical infrastructure, industrial robotics, and marine enclosures. Explore certified configurations directly produced at our Yueqing precision manufacturing plant.
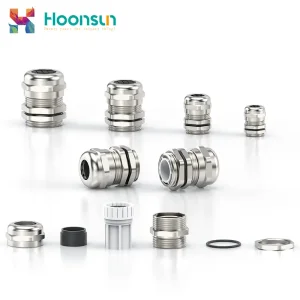
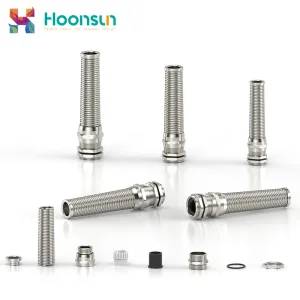
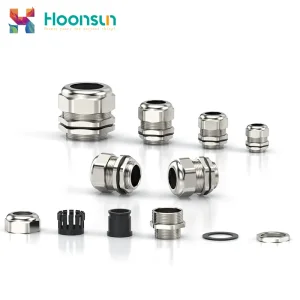
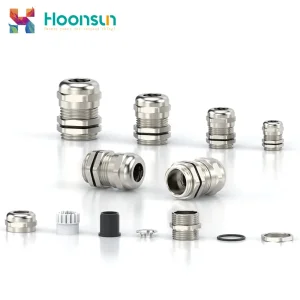
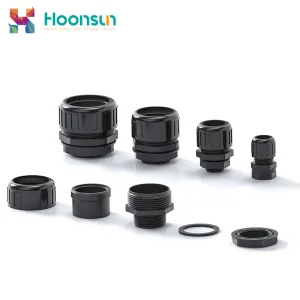
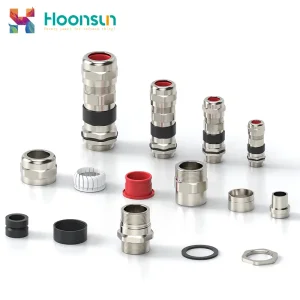
150mm² 4-Core Cable Geometry & Gland Sizing Architecture
A rigorous dimensional analysis of nominal conductor cross-sections, dielectric insulation, bedding tolerances, armor wire diameters, and final gland frame selection.
Demystifying the "150mm 4-Core Cable Gland Size" Search Intent
In electrical engineering, cross-sectional conductor area (150mm²) is often conflated with overall outer cable diameter (OD). A 4-core 150mm² low-voltage copper conductor cable (Cu/XLPE/SWA/PVC 0.6/1kV conforming to IEC 60502-1 or BS 5467) does not have an outer diameter of 150mm; rather, each 150mm² compacted stranded phase conductor has an approximate diameter of 14.5mm to 15.0mm. When assembled with XLPE insulation, inner bedding, galvanized steel wire armor (SWA, typically 2.5mm wire gauge), and an extruded outer protective sheath, the actual cable Outer Diameter (OD) typically falls between 52.0mm and 61.5mm.
Consequently, the mathematically and mechanically appropriate cable gland size for terminating a 150mm² 4-core armored cable is typically an ISO Metric M63 (M63 × 1.5) or an M75 (M75 × 1.5) frame, which corresponds to British Standard CW63 / BW63 / E1W63 or Imperial 2-1/2" NPT conduits. Sizing errors occur when specifiers confuse nominal conductor area with overall mechanical clamping diameters, leading to field entry failure, inadequate earth fault loop impedance, and moisture ingress.
| Cable Configuration | Voltage Rating | Armour Type | Nominal Cable O.D. | Recommended Metric Gland | Recommended BS Standard | Sealing Seal Range |
|---|---|---|---|---|---|---|
| 4 × 150 mm² Cu / XLPE / PVC | 0.6 / 1.0 kV | Non-Armored (Unarmored) | 46.5 – 51.5 mm | M63 × 1.5 | A2-63 | 44.0 – 54.0 mm |
| 4 × 150 mm² Cu / XLPE / SWA / PVC | 0.6 / 1.0 kV | Steel Wire Armoured (SWA) | 54.0 – 59.8 mm | M63 × 1.5 (Standard) | CW63 / E1W63 | 53.0 – 62.0 mm |
| 4 × 150 mm² Cu / XLPE / STA / PVC | 0.6 / 1.0 kV | Steel Tape Armoured (STA) | 52.5 – 58.0 mm | M63 × 1.5 | CW63 / Double-Seal | 51.0 – 60.0 mm |
| 4 × 150 mm² Cu / XLPE / SWA / LSZH | 0.6 / 1.0 kV | Heavy SWA + Fire Barrier | 57.5 – 63.5 mm | M75 × 1.5 (Oversize) | CW75 / E1W75 | 59.0 – 68.0 mm |
| 4 × 150 mm² Flexible Rubber Trailing | 0.6 / 1.0 kV | Heavy Duty Tough Rubber | 58.0 – 65.0 mm | M75 × 1.5 | A2-75 / Anti-Bending | 57.0 – 66.0 mm |
Thermal Expansion Under 430A Full Load
A 150mm² 4-core copper feeder regularly conducts 350A to 430A per phase under full load, driving operating core temperatures up to 90°C. Factory-engineered cable glands utilize compound vulcanized silicone or EPDM elastomers that retain mechanical memory under continuous thermal cycling.
- Zero compression set across -40°C to +120°C
- Eliminates inner insulation cold creep
- Prevents long-term ingress degradation
360° Armor Clamping & Earth Fault Continuity
For steel wire armored (SWA) cables, the gland's internal armor cone and clamping ring must deliver low-resistance metallic bonding. In the event of a high-voltage transient or phase-to-earth fault, the gland safely conducts thousands of amperes into the switchboard earth bar.
- Tested short-circuit current withstand >13.3kA / 1s
- Cast brass locknuts prevent vibrational back-off
- Integrated brass earth tags avoid galvanic hot spots
Mechanical Retention & Pull-Out Resistance
Heavier 150mm² 4-core cables impose severe cantilever deflection and axial tensile loads on junction boxes. Our CW63 and M63 gland housings exceed IEC 62444 Class A and Class B retention standards, exceeding 1,200 Newtons of mechanical pull-out force resistance.
- Reinforced clamping teeth on armor cone
- Deep thread engagement (minimum 8 full turns)
- UL94-V0 flammability rated sealing rings
Why Sourcing from Yueqing Precision Factories Maximizes ROI
Located in Liushi, Yueqing—China’s global capital of low-voltage electrical apparatus—HOONSUN (Zhejiang Hongxiang Connector) leverages an integrated industrial ecosystem to outperform global benchmarks.
Dedicated CNC Machining
Unlike assemblers who buy generic parts, our workshop operates automated multi-axis CNC machines and precision lathes turning high-purity CW614N brass bar stock into bodies and nuts with +/- 0.02mm tolerances.
Automated Electroplating
Continuous automated nickel plating delivers an impenetrable 5-8 micron coating. This barrier guarantees over 480 hours of salt spray resistance (ASTM B117), impervious to atmospheric sulfur and coastal corrosion.
Direct Raw Material Supply
Immediate proximity to domestic copper refineries and raw polymer extruders insulates our production pipeline from speculative metal spikes, passing a direct 30-45% cost efficiency to international EPC clients.
100% In-House Batch Testing
Every production lot is subjected to hydrostatic pressure testing (IP68 @ 10 bar), tensile strain resistance testing, armor clamp continuity checks, and optical thread pitch verification before customs packaging.
Metallurgy, Chemical Resistance & Sealing Integrity
Selecting the optimal gland metallurgy and elastomer compound is as critical as dimensional sizing when deploying 150mm² 4-core power feeders in corrosive or demanding environments.
CuZn39Pb3 (CW614N) Nickel-Plated Brass
The global standard for industrial power plants, switchboards, and factory substations. Features superior tensile strength (450 MPa) and machinability. The electrolytic nickel plating (Ni > 99.9%) prevents galvanic cell reactions between the brass housing, aluminum or steel mounting plates, and copper ground conductors.
- Standard: BS EN 12164 / CW614N
- Hardness: 110 - 150 HV
- High thermal conductivity dissipates cable heat
AISI 316L (EN 1.4404) Marine Stainless Steel
Mandatory for offshore drilling units (MODUs), wind turbine nacelles, chemical processing, and coastal splash zones. Molybdenum content (2.0 - 2.5%) provides immunity to chloride pitting, crevice corrosion, and acidic aerosol mist. Eliminates the risk of galvanic zinc de-alloying seen in untreated brass.
- Pitting Resistance (PREN): ≥ 23.5
- Continuous operating limit: -60°C to +300°C
- Ultimate tensile strength: > 580 MPa
Engineered Elastomeric Sealing Compounds
The seal ring makes direct 360-degree contact with the cable outer jacket. While budget suppliers use cheap reclaimed rubber that cracks under ozone exposure, our factory produces high-grade synthetic elastomers tailored to environmental factors.
- Neoprene (CR): General weather and oil resistance
- Silicone (VMQ): Extreme thermal extremes (-60°C to +200°C)
- Viton (FKM): Hydrocarbon, solvent, and acid immunity
Macro Industry Solutions: Heavy Industrial Applications
150mm² 4-core cables carry the bulk power that fuels modern industrial operations. See how our specialized glands deliver uncompromising sealing integrity across critical sectors.
Utility-Scale Solar PV & BESS Systems
In 1500V DC central inverter skids and containerized Battery Energy Storage Systems (BESS), 150mm² 4-core AC feeder cables require IP68 ingress protection against dust storms and heavy condensation, combined with UV-stabilized sealing rings.
Wind Power Generation Nacelles
Offshore wind towers subject heavy power cables to constant torsion, vibration, and saline air. Our marine TJ-clamping and anti-bending glands prevent conductor fatigue at the base of the tower and inside nacelle bus ducts.
Oil & Gas Petrochemical Refineries
In flammable hydrocarbon atmospheres, our double-sealed flameproof Ex d / Ex e cable glands isolate sparks, prevent explosive gas propagation along inner cable beds, and provide rugged mechanical protection against heavy pipe impacts.
Heavy Mining & Tunnel Boring (TBM)
Underground machinery utilizes flexible 150mm² trailing rubber cables subjected to rockfall, mud slurry, and extreme dragging forces. Strengthened brass glands with heavy external clamping saddles prevent cable slippage and tearing.
Overcoming Global Procurement & Thread Incompatibilities
A major failure point in international switchgear imports is thread mismatch between gland plates and gland bodies. HOONSUN engineers custom thread geometry to match any regional or project specification.
ISO Metric Threads (M63 × 1.5 / M75 × 1.5)
Conforming to ISO 965-1 and IEC 62444. Standardized across Europe, China, the Middle East, and APAC. Features a 60° thread angle with a standard 1.5mm pitch. Available with extended thread length (up to 20mm) for thick cast-iron explosion-proof enclosures or non-metallic composite walls.
National Pipe Taper (2-1/2" & 3" NPT)
Conforming to ANSI/ASME B1.20.1. Essential for North American infrastructure, oil refineries, and UL 508A industrial control panels. Features a 1° 47' taper angle that creates a pressure-tight mechanical wedge seal along the thread flanks, preventing flame propagation.
British Standard Pipe (G / BSPP) & PG Threads
Conforming to ISO 228 (parallel thread) and DIN 40430 (Panzergewinde: PG42, PG48). Widely specified in legacy German equipment, marine retrofits, and British Standard heavy industrial plants. Supplied with matching brass locknuts and chemical-resistant NBR O-rings.
Procurement Verification Checklist for Overseas Engineering Buyers
When issuing Requests for Quotation (RFQs) for 150mm² 4-core cable glands, procurement teams must verify the following five technical data points to prevent site installation rejections:
- 1. Exact Cable Outer Diameter: Confirm with cable datasheet whether O.D. is within 53-60mm (M63) or 60-65mm (M75).
- 2. Inner Bedding Diameter: For E1W double-seal glands, provide diameter under the armor wire to match internal elastomeric seal.
- 3. Enclosure Wall Thickness: Heavy cast enclosures require 18-20mm thread length instead of standard 12-15mm.
- 4. Clearance Hole or Tapped Entry: Clearance holes require brass locknuts and serrated shake-proof washers.
- 5. Operating Ambient & Ingress: Determine if installation demands standard IP68 (water immersion) or IP69K (high-pressure washdown).
Factory Floor Auditing & Quality Traceability
Take an inside look at HOONSUN’s (Zhejiang Hongxiang Connector Co., Ltd.) manufacturing infrastructure in Yueqing, verified by third-party testing labs and international exhibitions.
High-Tech Enterprise Credential
Recognized as a certified National High-Tech Enterprise since 2018. We operate clean-room assembly cells, automated digital torque testing fixtures, and strict optical gauge thread checking for zero-defect production.
International Exhibition Presence
Meet our senior technical engineering directors regularly at the Canton Fair (Industrial Automation Phase 1, Booth 20.1G03) and Middle East Energy Dubai (Electrical Distribution Zone, Stand B55).
Full CE, UL & RoHS Compliance
Every cable gland shipped carries complete technical documentation, including raw material chemical spectral analysis, UL yellow card compliance for nylon PA66, and CE low-voltage directive declaration.
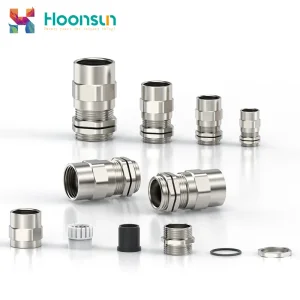
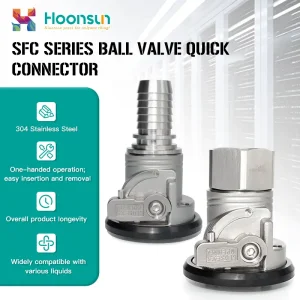
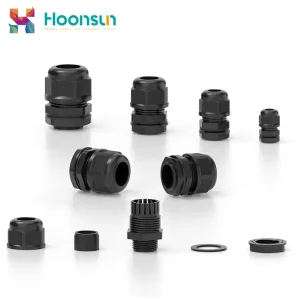
Advanced Sealing, Marine, & Heavy Armor Products
Explore our extensive range of specialized cable entry solutions, explosion-proof fittings, and high-flow quick disconnect couplings manufactured to international standards.
Engineering Inquiries & Sizing FAQ
Authoritative technical answers to critical sizing, earthing, certification, and mechanical questions asked by industrial plant designers and procurement directors.
What is the exact gland size for a 150mm² 4-core armored cable?
For a standard 0.6/1kV copper XLPE/SWA/PVC 4x150mm² cable, the overall outer diameter (OD) is typically between 54.0mm and 59.8mm. The corresponding industry standard cable gland is an ISO Metric M63 (CW63 / E1W63) with a clamping range of 53.0mm to 62.0mm. If the cable features an oversized fire-retardant LSZH outer sheath or steel tape armor exceeding 60mm OD, an M75 (CW75) gland must be specified.
What is the difference between BW63, CW63, and E1W63 glands?
BW63 is a single-piece, two-part dry gland designed for indoor armored cable terminations where no environmental moisture barrier is required. CW63 features a single elastomeric outer seal providing IP66/IP68 weatherproofing over the external cable sheath while clamping the armor. E1W63 is a premium double-compression gland providing both an internal seal over the bedding and an external seal over the outer jacket, preventing moisture tracking into the cable core.
Can you provide NPT threaded entries for American enclosures?
Yes. As a direct manufacturer, our Yueqing CNC lines machine custom thread forms to order. For 150mm² 4-core cables, we supply 2-1/2" NPT and 3" NPT male entry threads conforming to ANSI/ASME B1.20.1, complete with UL certification testing and hazardous location approvals for NEMA 4X switchboards.
How does HOONSUN validate continuous IP68 waterproof ratings?
IP68 under IEC 60529 requires dust-tight protection and continuous submersion under agreed parameters. HOONSUN tests its M63 and M75 heavy glands in submerged hydraulic pressure vessels up to 10 bar (approx. 100 meters water head) for 30 days. Protection is maintained when the cable outer diameter is properly matched to the seal range and the nut is torqued per catalog specifications.
Is brass plating mandatory, or is bare brass acceptable?
While bare brass is acceptable in clean dry indoor environments, nickel plating (5-8µm) is strongly recommended for 150mm² industrial connections. The nickel barrier prevents atmospheric oxidation, stops galvanic corrosion when clamped to aluminum or zinc-coated panels, and reduces thread galling when torqueing large M63 cap nuts (typically 120-140 Nm).
What is the standard production lead time for container orders?
We maintain an inventory of standard raw CW614N brass forgings and PA66 molding pellets. Standard catalog Metric M63 and M75 cable glands can be dispatched within 7 to 10 working days. Full container load (FCL) orders of 50,000+ units or custom NPT/Marine 316L runs are typically delivered in 20 to 25 calendar days FOB Ningbo or Shanghai.
Specify Engineered Industrial Cable Glands Direct from the Factory
Send your 150mm² 4-core cable technical datasheet, enclosure entry schedules, or custom OEM drawing to our engineering department. Receive verified 3D CAD step files, formal compliance test reports, and factory-direct volume pricing within 24 hours.